CPC
LLIBS

The objective of preparative chromatography is not to produce the most attractive chromatogram. It is to manufacture material at the required purity and recovery at the lowest practical cost per kilogram.
The cost per kilogram of purified product normally contains four major elements:
The main cost components are:
Loading describes the amount of sample introduced relative to the quantity of stationary phase. In packed-column chromatography, it is typically expressed as grams of sample per gram of silica. In CPC, it is expressed as grams of sample per millilitre of stationary-phase volume.
Higher loading distributes the operating cost of each cycle over more product. If loading is doubled under otherwise identical conditions - and the process produces twice as much acceptable product - labour, equipment, stationary-phase and solvent costs per unit of product may be approximately halved. The crude-material cost is not halved because twice as much feed is processed.
Loading cannot, however, be increased indefinitely. Above a certain point, separation deteriorates and yield begins to decline. The economic loading limit is therefore not simply the highest amount the system can accept, but the loading that produces acceptable purity at the lowest total cost per kilogram.
Initially, loading can be increased without a significant loss in purity or yield. Beyond a certain point, however, the chromatographic bands begin to overlap and first-pass yield decreases.
This does not automatically mean that the column is overloaded beyond its useful operating range. Accepting a lower percentage yield may still be economically advantageous if the higher loading produces more specification-grade product per cycle and the mixed fractions can be recycled. The real limit is therefore not the point where yield first declines, but the point where additional loading no longer reduces the total purification cost per kilogram.
Suppose one chromatographic cycle processes 25 mg of sample and recovers 22.5 mg of specification-grade product. If the same system can process 100 mg and recover 66 mg in a comparable cycle, the second run produces almost three times more product.
The feed cost increases because more material is injected. However, equipment time, labour and stationary-phase use per cycle may remain approximately constant. Mobile-phase consumption may also remain similar unless higher loading creates wider fractions or requires a longer method.
The total cost does not automatically fall in direct proportion to loading. Nevertheless, the fixed and cycle-related cost per gram of product can decrease substantially.
A basic productivity expression is:
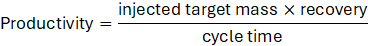 This explains why maximum recovery and maximum productivity do not necessarily occur at the same loading.
At low loading, the injected compounds occupy only a small proportion of the available stationary-phase capacity. Retention is approximately independent of concentration, and product recovery initially increases in proportion to injected mass.
As loading rises, the system enters a nonlinear operating region. The most concentrated part of a sample zone experiences different retention from its less concentrated edges. In packed-bed chromatography, the target and impurities may also compete for available interaction sites.
The practical consequences include:
This is not necessarily a process failure. Preparative chromatography routinely operates with overloaded bands because accepting some peak deformation can increase the amount of product manufactured per hour.
The relevant question is whether the additional product compensates for the loss in recovery and the cost of handling mixed fractions.
A LiLiChro application note demonstrates this relationship using a paraben separation.
At injection loads of 10 and 25 mg, the process achieved approximately 99% purity and more than 90% recovery. At 100 mg loading, recovery decreased to 66%.
Viewed only as percentage recovery, the 100 mg result appears inferior. The recovered product mass gives a different conclusion:
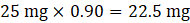
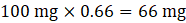 The higher-load run produces approximately 66 mg of acceptable product instead of 22.5 mg. Recovery decreases, but product output per cycle increases by almost threefold.
Whether this operating point is more economical depends on cycle time, solvent consumption, fraction volume and the destination of the unrecovered target. The loading decision cannot be made from yield alone.
Request the full study at our site: lilichro.com/#contact
Increasing loading usually creates a central product fraction and adjacent mixed fractions containing both target and impurities. These mixed fractions may be returned to the process if their composition remains suitable.
A recycle fraction should have:
Material entering a recycle fraction is not recovered product. Its value should be reduced by the additional labour, solvent, equipment time and potential degradation associated with another cycle.
Loading must be increased experimentally using representative crude material. For every injection, record:
The optimum is the loading that gives the lowest total cost per unit of acceptable product. It may occur after peak distortion begins and after percentage recovery starts to fall.
Stopping at the highest-yielding injection can leave much of the equipment’s productive capacity unused. Increasing loading too far can create excessive recycle, solvent consumption and product loss. Preparative method development must locate the economically useful point between these extremes.
The next practical question is whether this optimized amount can be introduced into the system without precipitation, breakthrough or loss of sample-zone focusing.